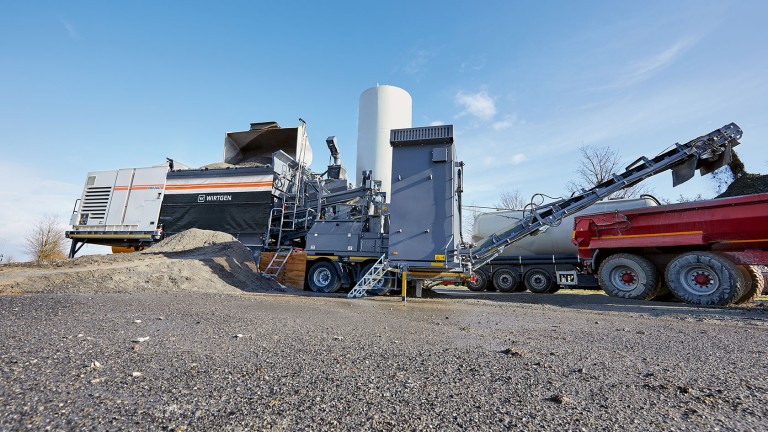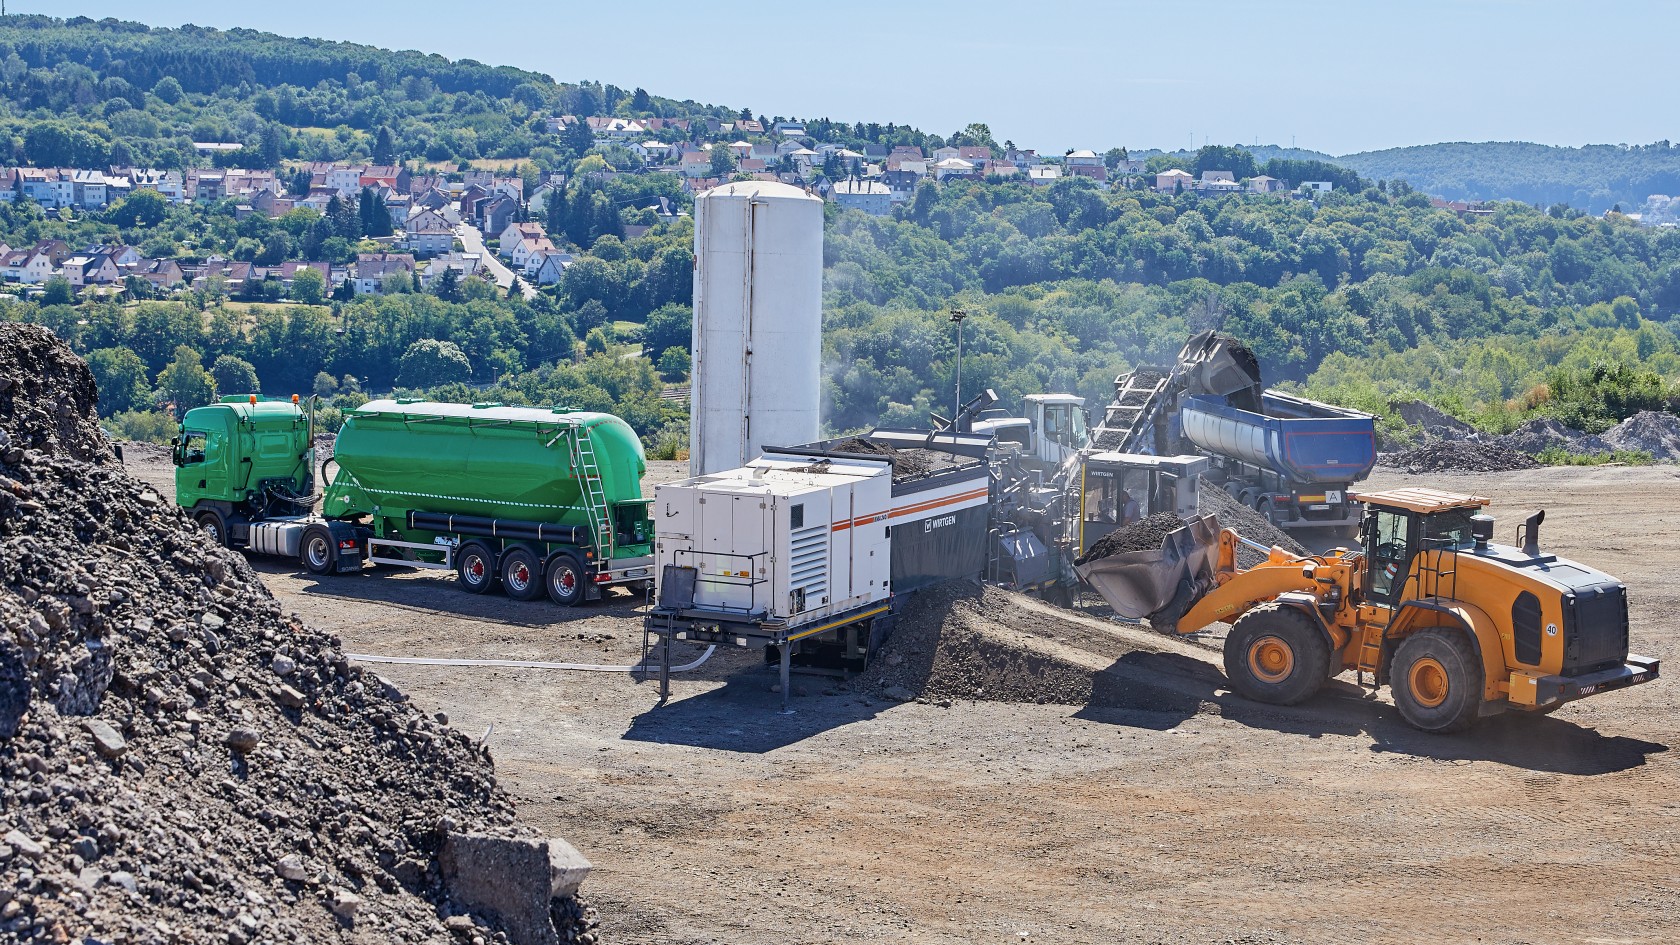
Mixing close to the construction site.

The Wirtgen cold recycling mixing plant KMA 240(i) expands the range of applications.

The Wirtgen Group offers a variety of solutions for the recycling and re-use of road construction materials such as milled material reclaimed during the removal of asphalt pavement in the course of road rehabilitation projects. One of these solutions is the mobile cold recycling mixing plant. KMA 240(i). This high performance plant from Wirtgen is an ideal choice for resource-efficient and economical production of asphalt mixes close to construction sites. It enables plant operating companies to convert up to 240 t of reclaimed pavement material into new, high-quality paving mixes per hour.

Optimum material flow in a perfectly coordinated system: Learn more about how a Wirtgen cold recycling mixing plant KMA 240(i) works.

Production of a variety of construction materials ranging from bitumen-bound mixes to cement-treated base layer mixes.

Mounted on a low-loader semi-trailer, and equipped with its own engine unit, the new cold recycling mixing plant KMA 240(i) can be quickly and easily moved to a location close to a construction site and begin production more or less right away. Whenever necessary, the mobile concept enables flexible relocation of the plant to a wide variety of locations. These proven advantages were also characteristic features of its predecessor from Wirtgen, the KMA 220(i). The engineers from Wirtgen have further developed, revised and upgraded the performance and precision of the plant The outstanding features of the new KMA 240(i) include higher mixing performance and an innovative cement dosing system with automatic self-calibration controlled by static weighing. Fresh bitumen is added to the mix in the form of bitumen emulsion or foamed bitumen.

Thanks to its powerful six-cylinder diesel engine, the new, high-performance cold recycling mixing plant from Wirtgen can convert up to 240 t of reclaimed asphalt pavement material into high-quality mix per hour. On a full tank, the engine provides sufficient power for up to two days of exceptionally cost-efficient production of recycled mix from a wide range of non-cohesive base materials predominantly sourced from Wirtgen cold milling machines. Low emission values mean the plant can also be used on inner city sites. Thanks to the highly-effective soundproofing of the engine housing, plant operatives and local residents will particularly welcome the significant reduction of noise emissions.

Tolles Produkt

The hourly processing of 240 t means: 20 t of cold recycled mix every 5 minutes

Economical and versatile Cold recycling with the KMA 240(i)

With in-plant cold recycling, a mobile cold recycling mixing plant (Kaltrecycling-Mischanlage - KMA) is set up close to the construction site. This saves time, minimises the need for the movement of material by trucks and contributes to the efficiency of construction site procedures: Depending on the project specifications this can mean up to 60% lower CO₂ emissions through cold recycling, up to 50% shorter construction times and up to 50% lower construction costs.

The cold recycling mixing plant KMA 240(i) produces mix that can be paved immediately and is suitable for the production of various types of bound base layers. For example, it can produce mix for cement-treated base layers (CTB) and roller-compacted concrete (RCC) and bitumen-bound base layers by the addition of bitumen in the form of bitumen emulsion or foamed bitumen. The range of applications for the various mixes includes motorway construction, building roads and paths roads and the construction of car parks.

The new public and industrial infrastructures constructed in this way are characterised by a high load-bearing capacity, resistance to deformation and a long service life. Cold recycling technology from Wirtgen enables the re-use of up to 100% of the existing milled material and thus offers economically attractive savings potentials.

On the main control panel, the operator can keep an eye on the material flow diagram, machine status and the whole production process at all times.

The advantages in figures (project-dependent)
Recycling of existing RAP
as much as 100%
Reduction of material for disposal
as much as 100%
Reduction of project transport logistics
as much as 90%
Reduction of required resources
as much as 90%
Reduction of binding agents
up to 50%

The cutting-edge process technology of the KMA 240(i) enables faster mix production

Thanks to microprocessor controlled plant control, the KMA 240(i) works with exceptional precision. The plant is supplied with binding agents such as hot bitumen, bitumen emulsion and cement from storage silos or tanker trucks. The precise metering of the base materials and binding agents in proportions determined beforehand in a road construction laboratory is monitored by a tried-and tested microprocessor control system. Ideally, the KMA 240(i) then loads the new, homogeneous material mix directly into trucks or continuously deposits it on stockpiles.


The paving process with a cement-treated base layer (CTB)

5. paving
1. Milling + stabilisation
2. Transport / unloading
3. KMA 240(i)
4. Transport from the plant to the construction site

Case study: New CTB at Paderborn-Lippstadt Airport

During the rehabilitation of the apron and the refuelling and de-icing area of Paderborn-Lippstadt Airport, the requirements included not only a high mixing capacity, but also an increase in the compressive strength of the new cement-treated base layer (CTB). On this project – one its first real-world tests – the KMA 240(i) processed 5,500 t of construction material in only 7 days, producing ready-to-pave mix in the process.

Prior to this, the lead contractor, Oevermann, had already milled off the 15,000 m² tarmac surface of the project site with a Wirtgen cold milling machine W 220(i) and had stockpiled the removed material on an adjacent car park with crushed limestone 0/5 as an additive. A wheeled loader transferred both materials to the cold feed hopper of the KMA in a ratio of 80% milled material to 20% limestone, where they were combined with the binding agents cement and water in a twin-shaft pugmill mixer and processed into a high-quality mix.

Tolles Produkt

Up to 10% binding agent can be added

As a rule, the uniaxial compressive strength of such mixes is 5 – 7 MPa. In this case, however, the CTB needed to meet more stringent requirements and achieve a value of 12.5 – 15 MPa. The contractor operating the KMA 240(i) therefore decided to add a higher proportion of 10% cement to the material mix of milled granulate and limestone instead of the usual 5 – 6%. The ability to precisely adjust the feed rate of binding agents is one of the advantages of the more advanced features of the KMA 240(i) that extend its range of applications.

Thanks to the daily production of some 800 t of cement mix, the downstrean paving equipment was also in continuous use. After a Grader had spread the material evenly on the individual sections, two Hamm 3412 compactors ensured ideal compaction of the freshly-paved CTB.

For details and more information, please visit our product pages.