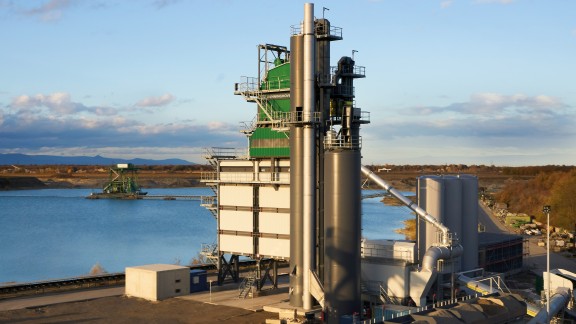
The catalyst in asphalt production
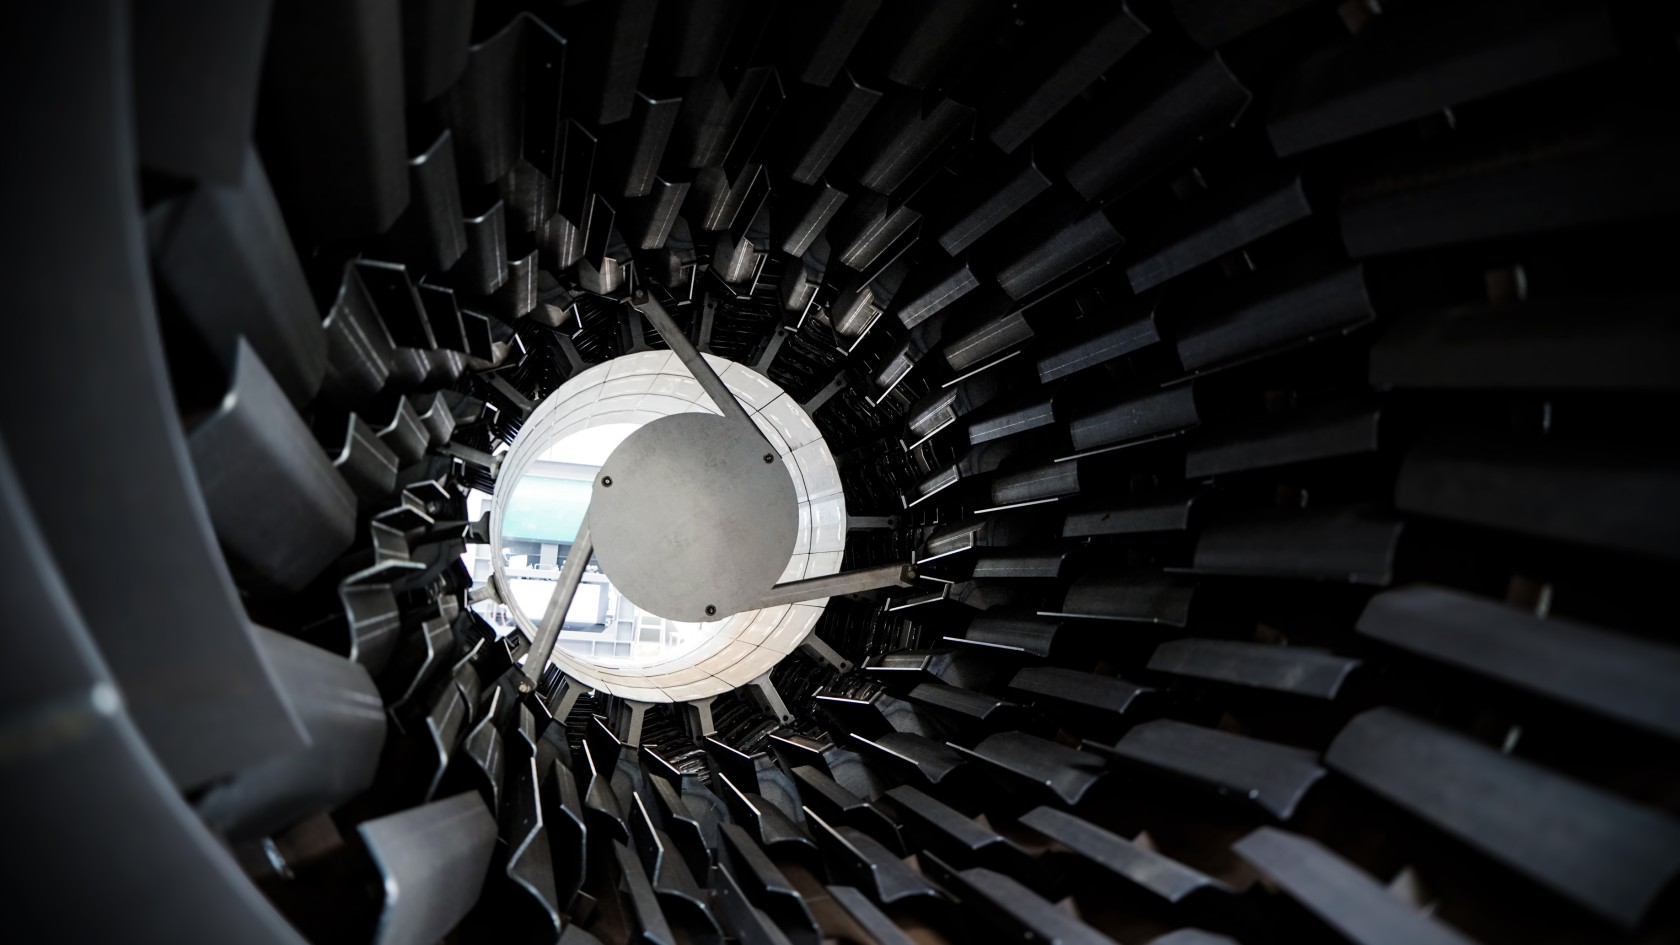

The Benninghoven REVOC system is a pioneering technology that gives plant owners the ability to achieve higher RAP material input rates while complying with stricter emissions limits.
The patented technology supplements existing cold and hot recycling systems in asphalt mixing plants and reduces total carbon emissions (TC) with up to 50% RAP material added. The specified limits of 50 mg/m³ are not exceeded.
The permissible emissions limits are being tightened up in many regions worldwide. Complying with these during asphalt production with RAP material is a challenge that plant owners have to tackle.
As soon as RAP material has to be added to the mixing process, complying with the permissible limits for total carbon (TC/VOC) from volatile organic compounds becomes a complex task. These VOCs are more potent greenhouse gases than CO₂ and are also hazardous to health at higher concentrations. Going forward, these emissions must be reduced as much as possible, to ensure existing asphalt mixing plants can stay in business and keep their operating permits.
The key advantage of the REVOC system is that it can help to secure the future of asphalt mixing plants, because of this added efficiency, the use of RAP material and the emissions parameters allow plant owners to maintain the foundation of their business in the future.
In particular, in light of the ever more restrictive requirements from government authorities, the REVOC system is the economical option for smooth operation.
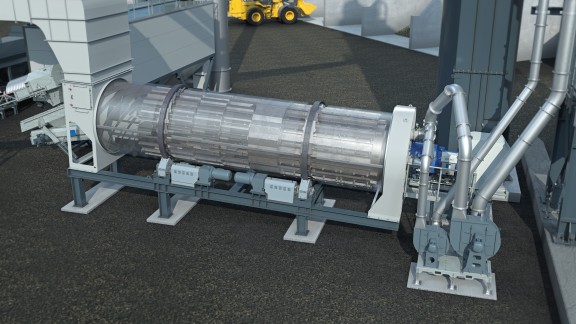
The BENNINGHOVEN REVOC system is an integrated process system. To reduce emissions and comply with standards and administrative regulations such as the German TA-Luft regulation, the entire process has to be considered: the burner, fuel, RAP feed systems, dedusting system, dryer drum dimensions, and REVOC system itself.
Emission values can meet or even exceed the required standards only if these factors are perfectly coordinated technically, and the plant is run exceptionally well by experts with the targets in mind.
First, exhaust gases are actively extracted directly where they are generated, primarily from the mixer in the asphalt mixing plant – where heated mineral, the RAP material, and the bitumen come together to be mixed into fresh asphalt. The fumes with high TC concentrations are then moved to the REVOC system for thermal processing.
The energy that is generated for drying and heating the virgin mineral (primary function) is used by the REVOC system to also burn off the total carbon (secondary function).
Using technology to work towards a more efficient use of energy and raw materials is the challenge of today and tomorrow. Solutions from Benninghoven can help to cut energy consumption and emissions, and enable the operation of asphalt mixing plants with high rates of RAP usage – which also ensures the long-term future of the mixing plant site.
Find out moreAsphalt production, recycling systems, combustion technology, control systems, and bitumen technologies – thanks to BENNINGHOVEN’s technologies, each of our customers can find the right solution for their specific site that fully complies with requirements and conditions.
Go to technologies