Fuels of the future
NEW

Flexibility for energy generation
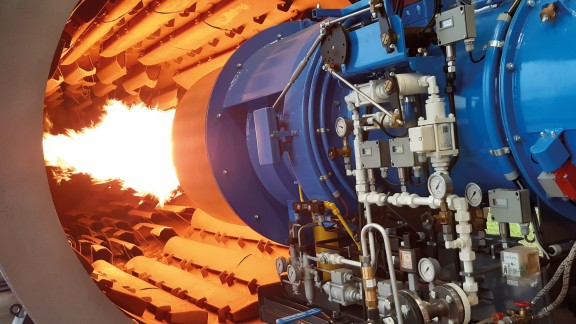
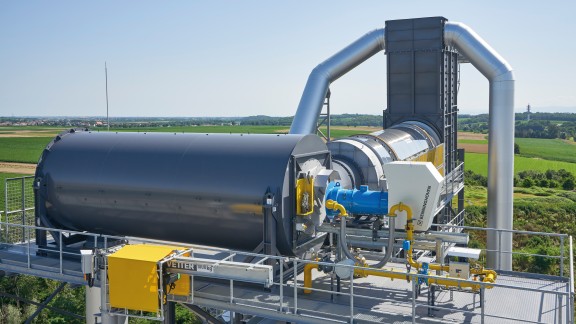
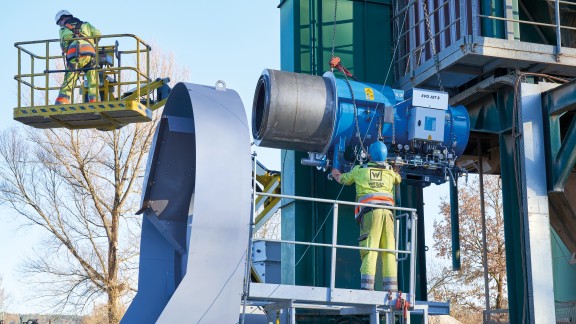
For any burner designed as a standard single-fuel burner for the drying and heating of the base material, there is the option of extending this burner to use up to three fuels. This conversion turns the burner into a multi-fuel burner that allows for a number of different fuel variants. This means that oil, natural gas, liquid gas and common gaseous substances such as DME or hydrogen as well as solids such as coal dust, BtL and wood dust can be combined.
This flexibility offers a number of benefits. On the one hand, this eliminates plant downtime due to delivery problems or a lack of raw material. On the other, the least-expensive fuel can always be selected in the event of price fluctuations affecting a particular fuel. In addition to this, the flexible use of alternative fuels enables drying without fossile CO₂ emissions. Overall, the burner increases the economic efficiency and flexibility of modern energy generation processes.
All over the world, climate action and tougher regulations from state and local governments are also challenging the asphalt industry to reduce its output of greenhouse gases like CO₂. Owners of asphalt mixing plants have to reduce emissions to help secure the future of the plant site. When it comes to mixing asphalt in a cleaner and more sustainable way, changing from oil or coal dust to gas is a major step:
In addition to fossil fuels, there is also an option to use renewable fuels such as wood dust and liquified biomass (biomass-to-liquid). Additionally, they are based on renewable raw materials and can support the diversification of fuel supply. In contrast, fossil fuels are finite resources that will not be available forever, which presents a challenge.
“We are always thinking ahead and developing solutions for tomorrow. Apart from enabling the use of future fuels such as wood dust, BtL and hydrogen, we also focus on direct energy savings.”
Steven Mac Nelly, Head of Development & Design Engineering at BENNINGHOVEN
Oil burner for light heating oil (heating oil EL)
Heating oil made from crude oil is divided into two types: light heating oil (heating oil EL) and heavy heating oil (heating oil S). The quality requirements for heating oil are defined in DIN 51603. Light heating oil can be burned in furnaces, central heating systems and industrial firing plants without preheating. Heavy heating oil, on the other hand, has to be preheated for transport and burning. The systems running on these fossil fuels, however, are increasingly subject to regulations and restrictions.
Liquid gas burner and natural gas burner
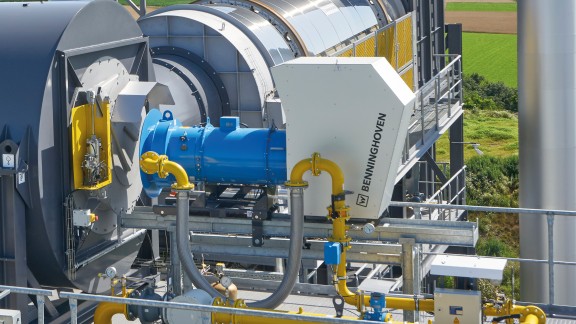
The BENNINGHOVEN gas burners can burn liquid gas already during the liquid phase, without first having to transform it into a gaseous state. This means that no additional periphery such as an evaporator is necessary and therefore no additional energy is required either.
Liquid gas burners and natural gas burners have the same mechanical structure. They differ only in their periphery, i.e. how the fuel is introduced into the burners.
Liquid gas, referred to as “associated gas”, is generated during the extraction of crude oil or natural gas. This associated gas used to be simply released into the atmosphere or burned in many cases. Today, more and more regions worldwide have banned this burning, which has an additional positive impact on the increasing availability of liquid gas.
Hydrogen drying system from BENNINGHOVEN
GAME CHANGER – the burner generation that can also use 100 % green hydrogen
* Energy-intensive thermal drying and heating process for virgin and RAP material, carbon-free thanks to green hydrogen.
Learn moreStill burning in the future
Wood dust can be used as a fuel from biogenic raw materials. With the MULTI JET wood dust burner, BENNINGHOVEN has made it possible to use wood dust in asphalt mixing plants and expanded the portfolio of its own burner technology.
The development engineers at BENNINGHOVEN have identified the ideal particle size of the wood dust, which is produced mainly from scrap wood and wood waste. Identifying the optimum grading curve for the fuel is important for the flame geometry of the burner – and therefore for the effectiveness of heating the virgin mineral or the recycled asphalt (RAP). Several Benninghoven customers are already successfully using the MULTI JET wood dust burner.
Investing in a solids burner entails a low risk and is future-proof as the burner design means that coal dust as well as wood dust can be used as fuels. This means that the burner can initially be run with coal dust and then later switched over to carbon-neutral wood dust. In light of the first supply bottlenecks for coal dust, wood is already becoming increasingly important as a sustainable fuel.
The complete periphery includes the burner and the dosing unit. The interface to the customer systems is the inlet to the dosing unit. The wood crusher and the wood silo are provided by the customer.
Burner
The wood dust is fed into the burner with precision dosing by means of the feed fan and the dosing unit. In the burner head, a separate auxiliary flame then ignites the material. The control range for wood dust with pilot flame is 1:6; the calorific value of wood dust is approx. 18 MJ/kg depending on the type of wood.
The secondary fuel, e.g. heating oil EL, liquid gas or natural gas, is used for the support flame.
The wood dust dosing system with storage tank has a capacity of 2.5 m³ and is installed at the discharge of the wood dust silo. In the tank, two agitators prevent the formation of bridges in the wood dust. A speed-controlled dosing screw releases the fuel in accordance with the required burner output and transports the wood dust into a blow-through rotary valve, which forms the interface to the conveying pipe. From there, the wood dust is blown into the head of the burner with a feeder fan and pipe.
Starting material on the asphalt mixing plant
The owner is obligated to ensure that the overall plant (for example the silo with the dosing system) is checked as part of a regular inspection as per the German industrial safety regulations (BetrSichV). Outside of Germany, the systems are subject to mandatory testing – the applicable national laws and directives must be observed.
Explosion protection (ATEX) especially for coal dust and wood dust
Energy from biomass
The principle of producing biomass-to-liquid (BtL) fuels is based on liquefying biomass.
In the case of wood as a starting material, thermo-chemical conversion processes in a reactor use high temperature and high pressure to turn the cellulose-rich wood into pyrolysis oil.
The further processing steps are cleaning, synthesis and refining of the pyrolysis oil to produce BtL fuels.
Another significant development in the energy market is the use of liquefied biomass (BtL). BtL can be produced from plant waste such as straw, wood or energy crops like maize and oilseed rape. BENNINGHOVEN now also offers an innovative
solution for the use of BtL as a fuel: the MULTI JET BtL burner. Like wood dust, biomass-to-liquid is also considered carbon-neutral. And like all MULTI-JET burners, BENNINGHOVEN BtL burners can also be run with other fuels such as oil, coal dust and gas. The new BENNINGHOVEN burners therefore offer plant operators a future-proof investment option: continuing to use fossil fuels in the short term while being ready to switch to renewable fuels quickly.
For wood or wood waste as a starting product, the challenge lies in the processing of the natural material that can vary greatly in its chemical composition. These fluctuations affect the final BtL product. Smaller fluctuations can be compensated by adapting the preheating temperature. Larger fluctuations or fuel changes, however, require adjustments on site.
Customers therefore send their heating medium to Wittlich in a stainless steel container so the correct basic parameters for the burner can be determined at the BENNINGHOVENBENNINGHOVEN factory for new fuels. There, the fuel is tested extensively and the optimum burner settings are identified.
Coal dust burner (brown coal or hard coal)
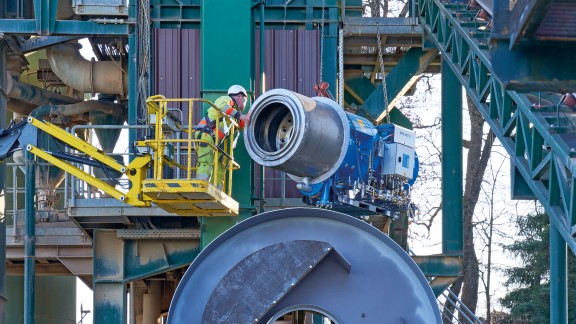
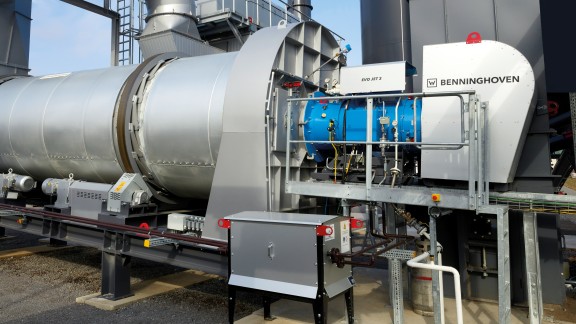
The BENNINGHOVEN MULTI JET burner, which is designed as an oil burner in standard models, can be expanded to utilise up to three other fuels. This turns the burner into a combination burner, which means that other types of fuel such as oil, natural gas, liquid gas, heavy oil, BtL fuels (liquefied biomass) and coal dust are all available as fuels. The lignite dust is fed into the feed pipe with the help of the coal dust dosing system (flange-mounted onto the outlet valve of the coal dust silo) and blown into the head of the burner by a conveyor fan.
This well-designed coal dust dosing system offers plant owners a number of key benefits:

Continuous material flow into the coal dust dosing line
CLF (continuous lignite flow)
> Low pulsation
> Constant, steady and uniform flame
> Clean flame – complete burning of the coal dust

Tested quality for a guaranteed process and functional reliability
> ATEX tested, TÜV certified
> The coal dust dosing system is manufactured in accordance with the new ATEX Directive (2014/34/EU) and has type approval: TÜV 19 ATEX 8337
> Approved for use in zone 21

Optimum customer benefit. Efficient and cost-effective, ensuring high usability and outstanding performance
> With the correct burner settings, coal dust is a clean fuel and the equal of any of the other fuels used for mineral heating
> Complies with the stringent requirements of TA Luft and all related technical codes

Optimum customer benefit. Efficient and cost-effective, ensuring high usability and outstanding performance
> Auxiliary flame switch-off at approx. 20% burner output
> Auxiliary flame consumption: reduced from 80 l/h to approx. 50 l/h
* pependent on BKS calorific value/quality in each case
Optimum customer benefit. Efficient and cost-effective, ensuring high usability and outstanding performance
> Vastly improved control range
> 1:8 with auxiliary flame, 1:5 for coal dust only
> Especially interesting for customers running a high RAP system rate, i.e. two burners run in parallel
> Enables the virgin mineral burner to be operated at a correspondingly optimised, economical rate
> Especially when taking into account the limited heat input of the burner(s) to 19.8 MW (German Greenhouse Gas Emissions Trading Act)
Using technology to work towards a more efficient use of energy and raw materials is the challenge of today and tomorrow. Solutions from Benninghoven can support the reduction of energy consumption and emissions while enabling asphalt mixing plants to run with a high reclaimed asphalt pavement (RAP) content to ensure the future of the facility.
Learn moreAsphalt production, recycling systems, combustion technology, control systems and bitumen technology – with BENNINGHOVEN technologies, every customer can find the right solution for their location, according to the specific requirements and conditions.
To the technologies